Capsule Container: Premium Packaging Solutions

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000

capsule container

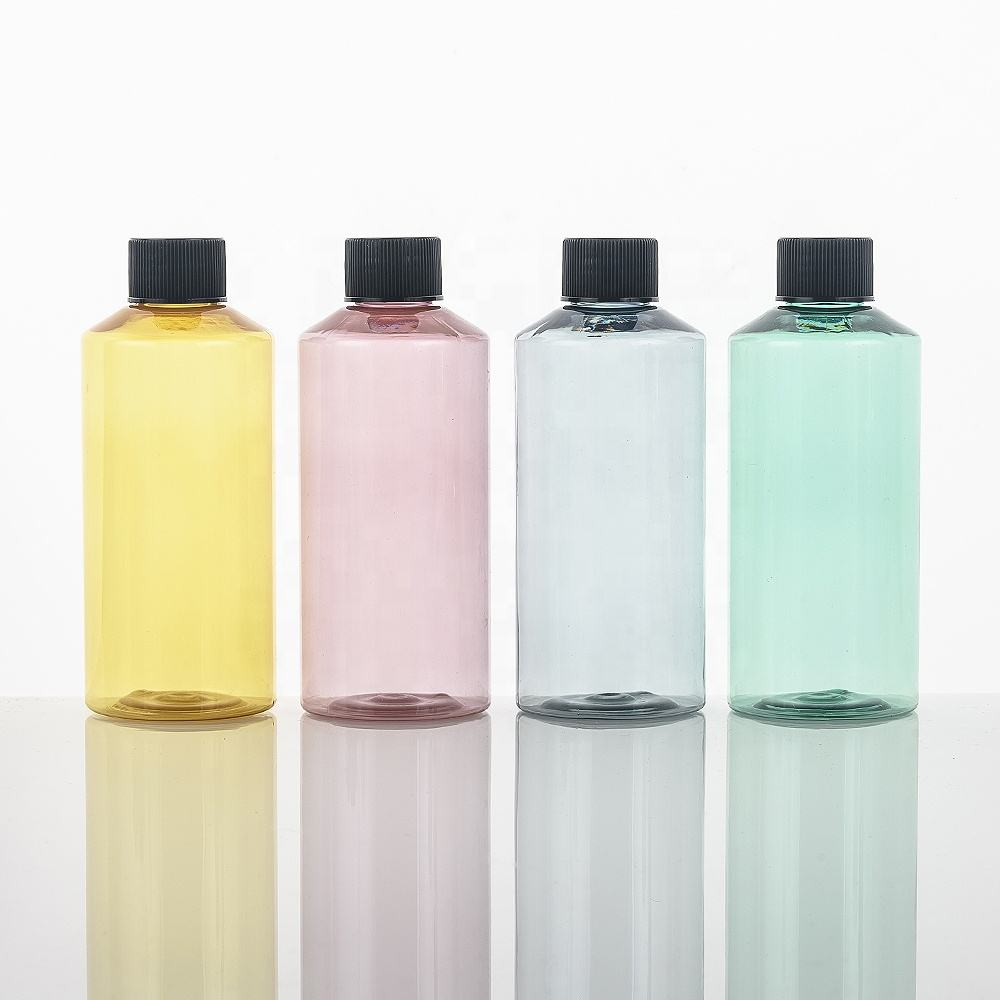
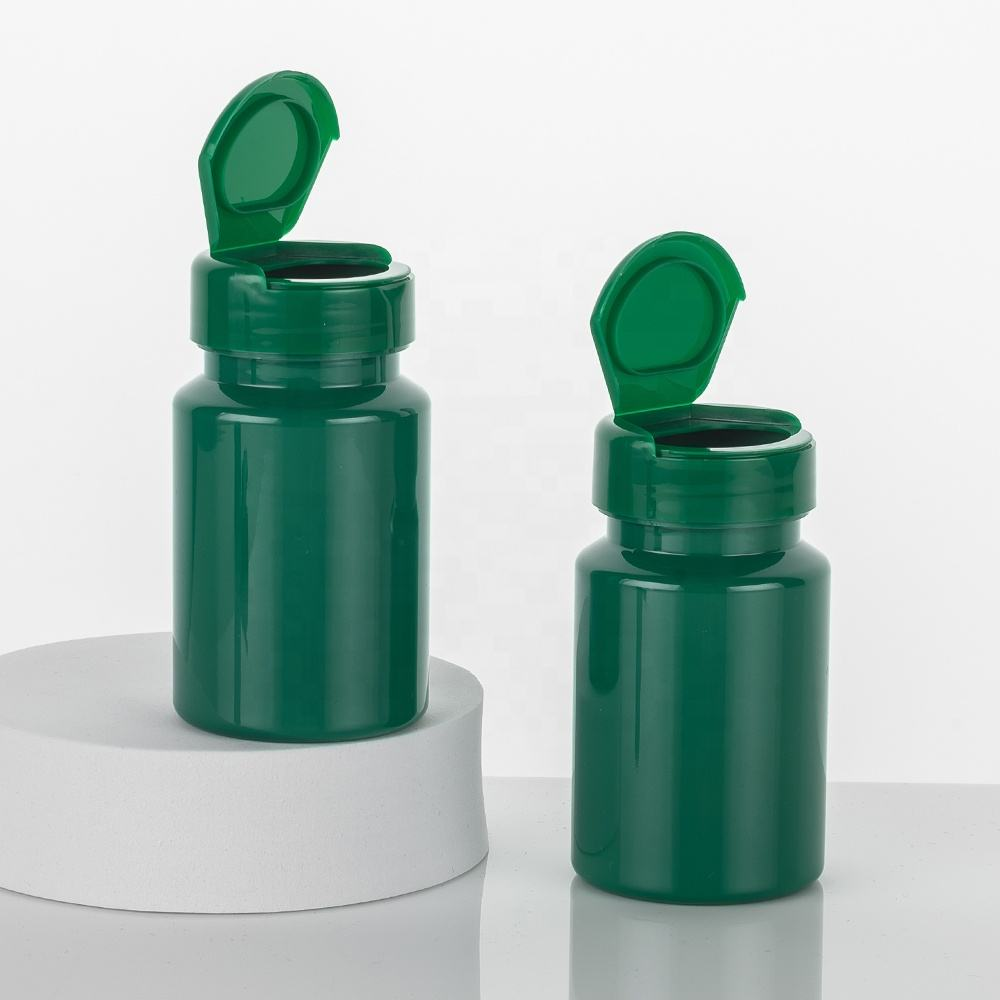
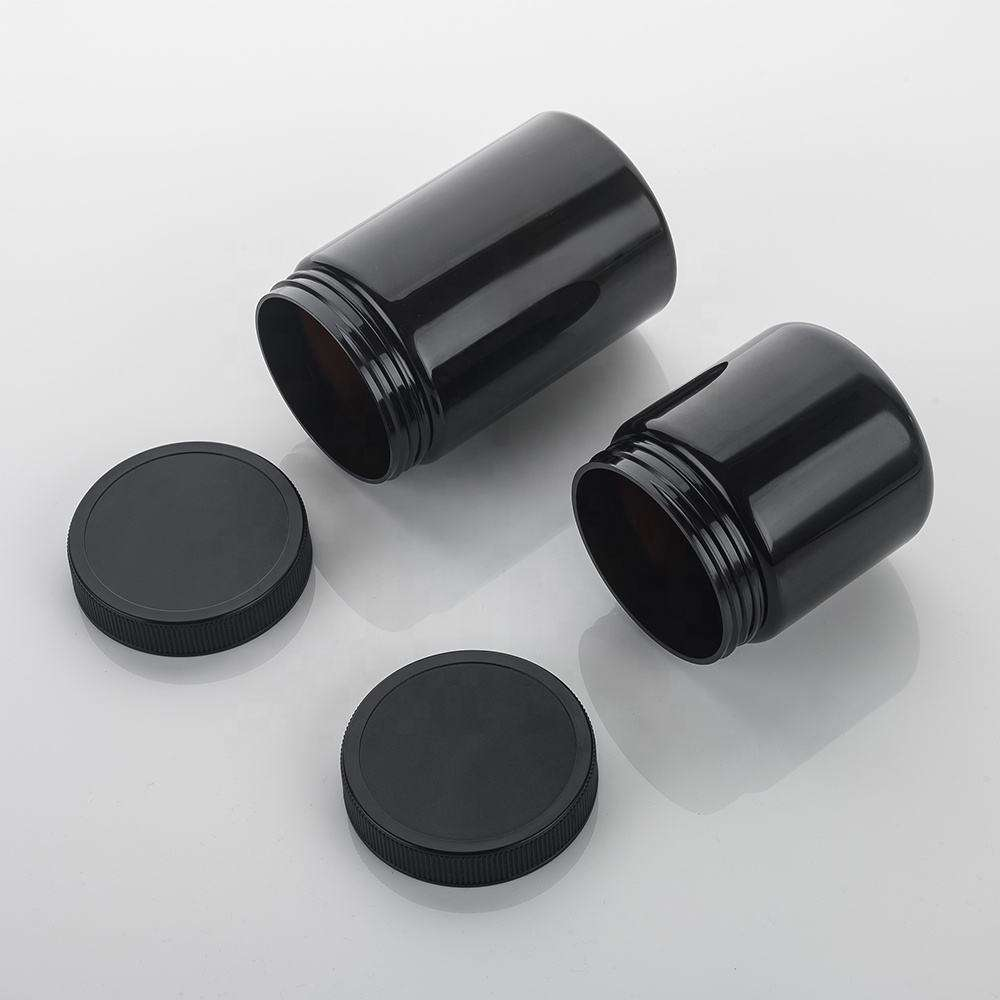
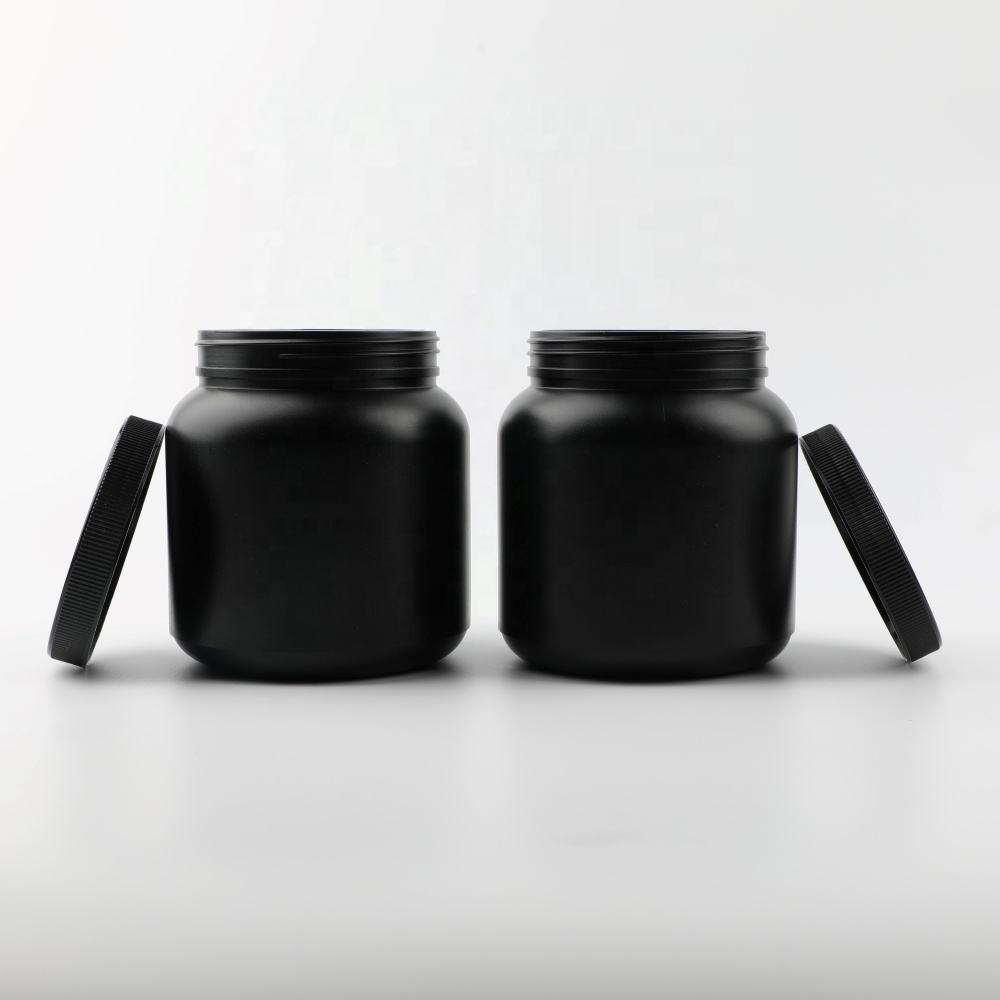
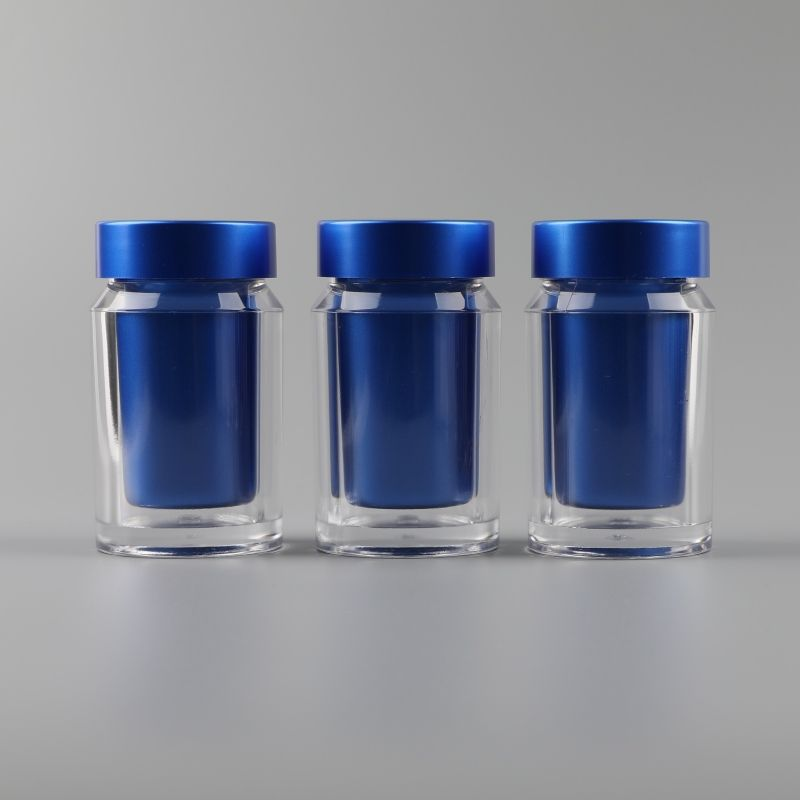
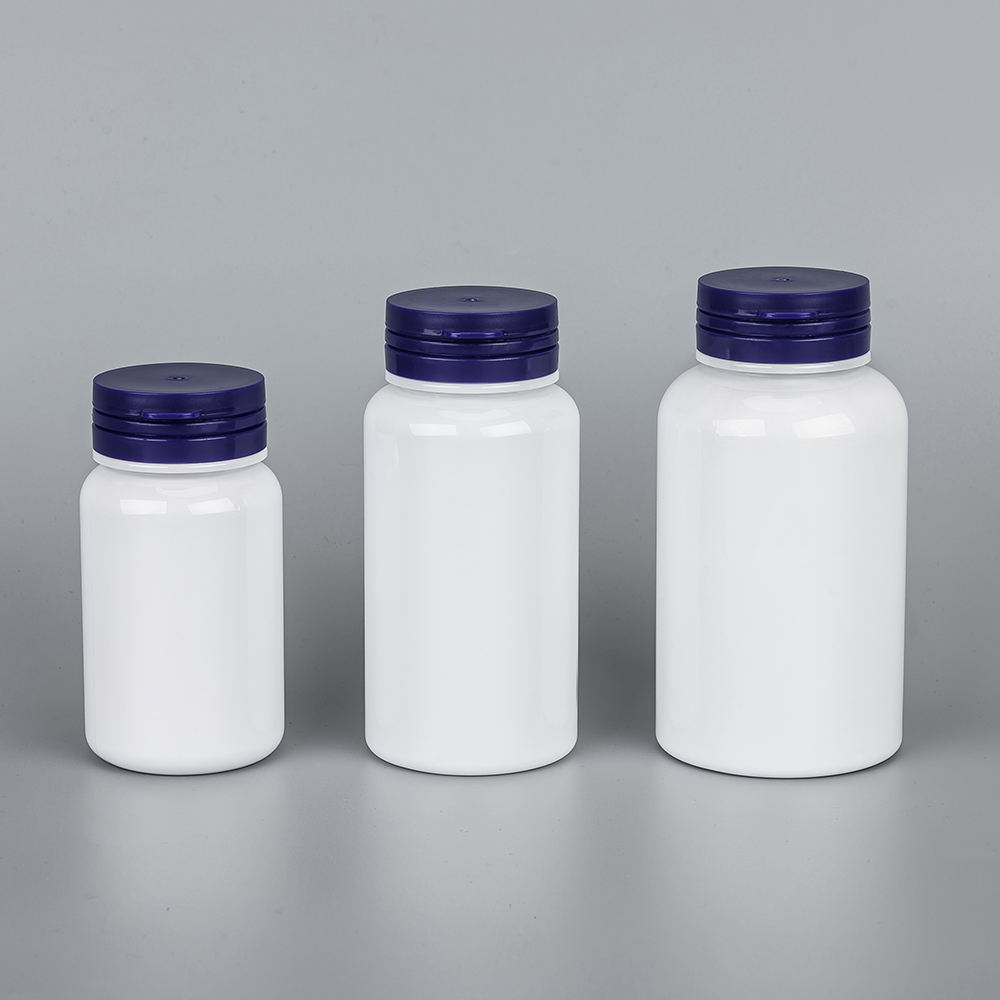
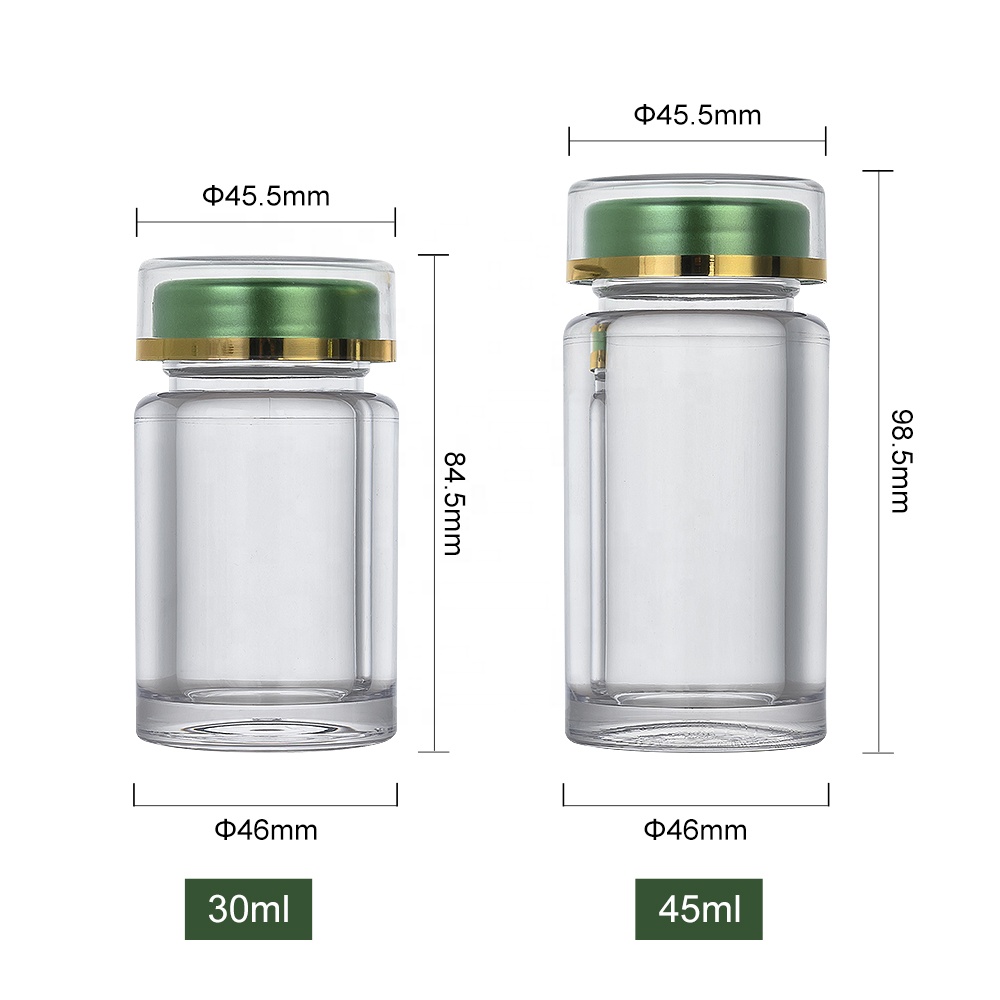
A capsule container represents a sophisticated packaging solution designed to preserve, protect, and deliver products with precision and excellence. This innovative capsule container serves multiple industries, from pharmaceuticals to dietary supplements and cosmetics, providing reliable containment for sensitive materials. The primary function of a capsule container is to safeguard contents from environmental factors such as moisture, light, and oxygen exposure, ensuring product integrity throughout storage and distribution. Modern capsule container technology incorporates advanced materials and design features that maximize protection while maintaining accessibility. The capsule container utilizes precision engineering to create airtight seals, preventing contamination and degradation of enclosed substances. Manufacturing processes for a capsule container employ high-grade polymers, glass, or specialized composites that meet stringent safety and quality standards. Technologically, the capsule container integrates features such as child-resistant mechanisms, tamper-evident sealing systems, and measurement capabilities for accurate dosing. Advanced capsule container designs often include oxygen absorbers, desiccants, and barrier coatings that extend shelf life significantly. The capsule container accommodates various product formats, including powders, liquids, and solid formulations. Applications for the capsule container span pharmaceutical delivery systems, nutraceutical packaging, cosmetic storage, and industrial material containment. The versatility of a capsule container makes it invaluable across sectors requiring superior product protection and controlled dispensing. Modern healthcare providers and manufacturers increasingly depend on capsule container solutions for maintaining product quality standards and meeting regulatory compliance requirements efficiently.

New Product Recommendations

The capsule container offers transformative advantages that directly benefit your business operations and customer satisfaction. First, a capsule container delivers exceptional product protection by creating an impermeable barrier against environmental degradation. Your valuable contents remain potent and effective longer, reducing waste and maximizing customer value from every purchase. Operationally, a capsule container streamlines your supply chain through standardized sizing and stacking efficiency. These containers optimize warehouse space usage, reducing storage costs significantly while maintaining accessibility for rapid fulfillment. The capsule container design simplifies inventory management, allowing your team to track stock levels with ease and accuracy. For your customers, a capsule container provides convenient handling and precise dosing capabilities. Whether consumers use your product daily or occasionally, the capsule container ensures consistent quality and safety with each use. The familiar capsule container format builds customer confidence and encourages repeat purchases through reliable performance. The capsule container demonstrates superior compatibility across diverse product categories. Manufacturers can utilize the same capsule container framework for multiple formulations, reducing production complexity and equipment investment. This flexibility accelerates time-to-market for new products while maintaining quality consistency. Regulatory compliance becomes simpler with a capsule container designed to meet international standards and safety certifications. Your capsule container solution eliminates costly redesigns and rejection issues, streamlining approval processes. Additionally, the capsule container enhances your brand image by demonstrating commitment to product excellence and customer protection. Finally, a capsule container offers exceptional cost-effectiveness compared to alternative packaging methods. The economies of scale in capsule container production translate into lower per-unit expenses without compromising quality, strengthening your profit margins while maintaining competitive pricing for consumers.

Practical Tips

What are the key dimensions for a standard 100cc capsule bottle?

08

Jul

What are the key dimensions for a standard 100cc capsule bottle?

When sourcing pharmaceutical or nutraceutical packaging, one of the most critical decisions a product developer or procurement specialist makes is selecting a container with the right dimensions. The capsule bottle is one of the most widely used pack...
View More
Why is a wide-mouth supplement container better for powders?

10

Jul

Why is a wide-mouth supplement container better for powders?

When sourcing pharmaceutical or nutraceutical packaging, the physical design of your chosen packaging matters far more than most people realize. The shape, the opening size, and the structural material of a supplement container directly affect how yo...
View More
What are the hidden benefits of an amber medicine bottle design?

28

Aug

What are the hidden benefits of an amber medicine bottle design?

The design of a medicine bottle might seem like a straightforward packaging decision, but the choice to use amber glass in pharmaceutical containers reveals a sophisticated understanding of chemical preservation and consumer protection. An amber medi...
View More
How to source a protein powder container with custom scoops?

22

Sep

How to source a protein powder container with custom scoops?

Sourcing the right protein powder container is a critical decision for supplement brands, fitness companies, and nutritional product manufacturers. The protein powder container serves as both a functional storage solution and a brand ambassador on re...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000

capsule container

Superior Environmental Protection

Superior Environmental Protection

The capsule container excels at shielding products from degradative environmental factors that compromise quality and efficacy. This protective capsule container design incorporates multi-layer barrier technology that blocks moisture infiltration, oxygen penetration, and light exposure simultaneously. The capsule container maintains stable internal conditions regardless of external humidity levels, temperature fluctuations, or storage duration. Pharmaceutical manufacturers rely on this capsule container protection to preserve medication potency, ensuring patients receive effective treatments. The capsule container's hermetic sealing technology prevents oxidation processes that would otherwise diminish product value. For sensitive supplements, cosmetics, and nutraceuticals, a capsule container provides the security needed for extended shelf life. Investment in quality capsule container packaging demonstrates respect for customer health and product integrity.
Convenient User Experience and Accessibility

Convenient User Experience and Accessibility

The capsule container transforms how customers interact with products through intuitive design and practical functionality. This user-friendly capsule container facilitates easy opening mechanisms while maintaining security through advanced closure systems. The capsule container accommodates measuring indicators for precise dosing, eliminating guesswork and ensuring consistent results. Visual transparency in many capsule container options allows customers to monitor product levels, supporting informed purchasing decisions. The portable capsule container format enables convenient carry-along usage for traveling professionals and active individuals. Ergonomic capsule container handles and grips accommodate users of varying physical abilities, promoting inclusivity. The standardized capsule container size simplifies storage in standard cabinets, refrigerators, and travel bags without wasteful packaging bulk.
Cost-Effectiveness and Operational Efficiency

Cost-Effectiveness and Operational Efficiency

The capsule container represents intelligent investment through demonstrated long-term economic advantages for manufacturers and consumers alike. Efficient capsule container production processes achieve significant economies of scale, reducing per-unit costs substantially. This affordable capsule container option enables competitive pricing while maintaining healthy profit margins for businesses. The capsule container's standardized specifications minimize customization expenses and accelerate manufacturing cycles. Reduced product spoilage through capsule container protection eliminates losses from expired inventory, improving financial performance. The capsule container design facilitates automated filling, sealing, and labeling, decreasing labor requirements and production timeframes. Companies adopting capsule container solutions report measurable improvements in operational efficiency, reduced waste percentages, and improved inventory turnover rates.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000