Capsule Container Manufacturers

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000

capsule container manufacturers

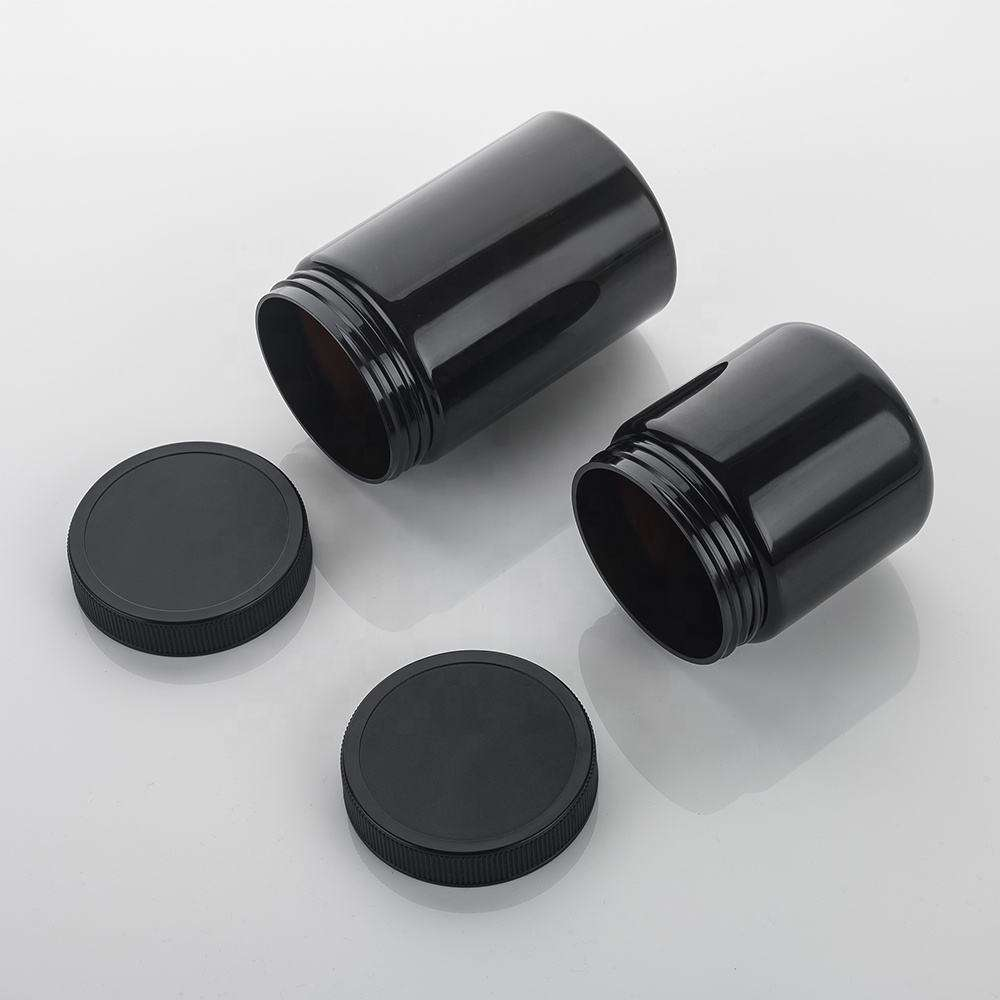
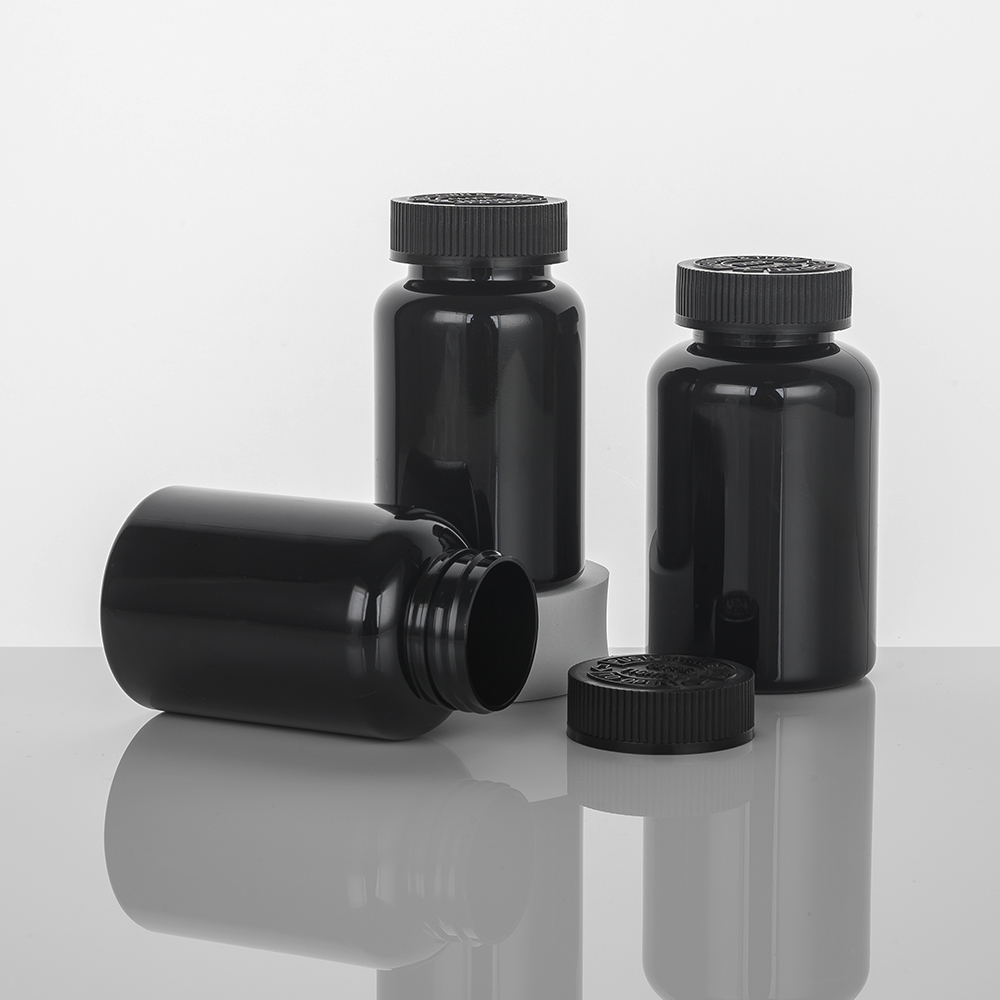
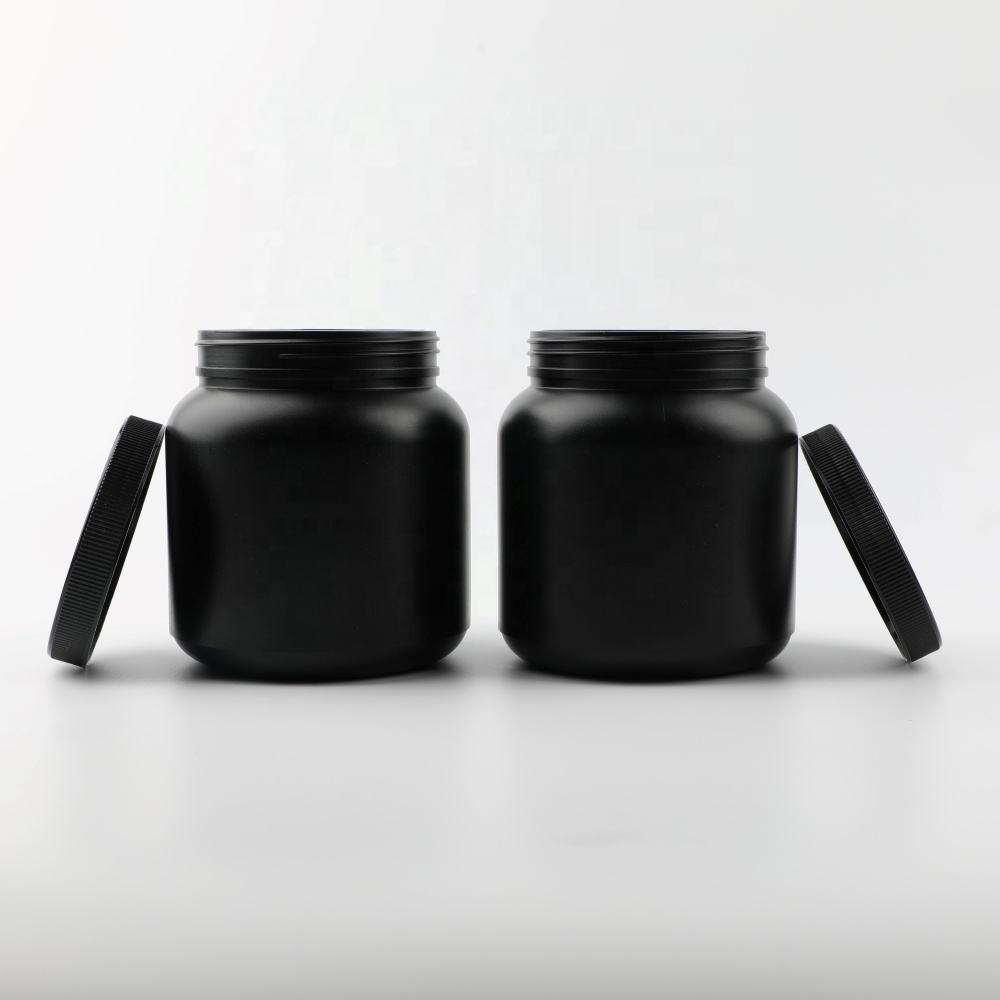
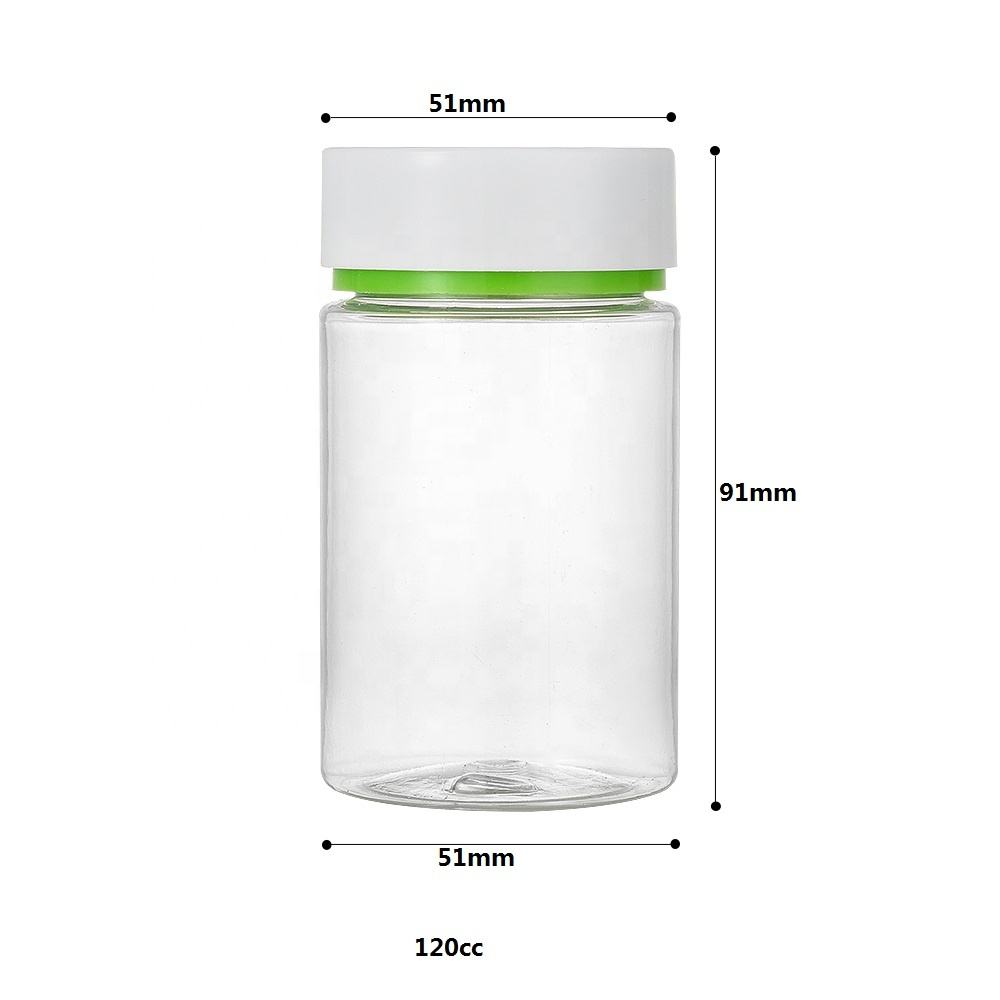
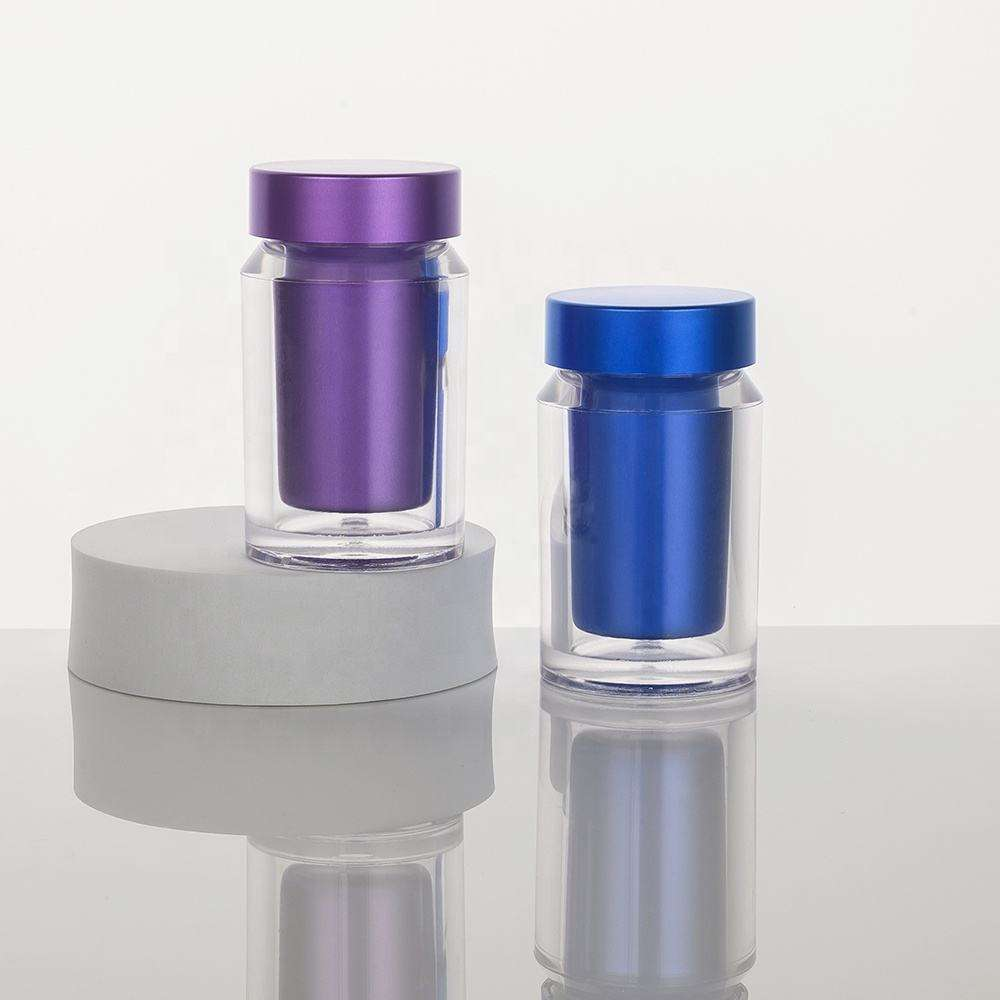
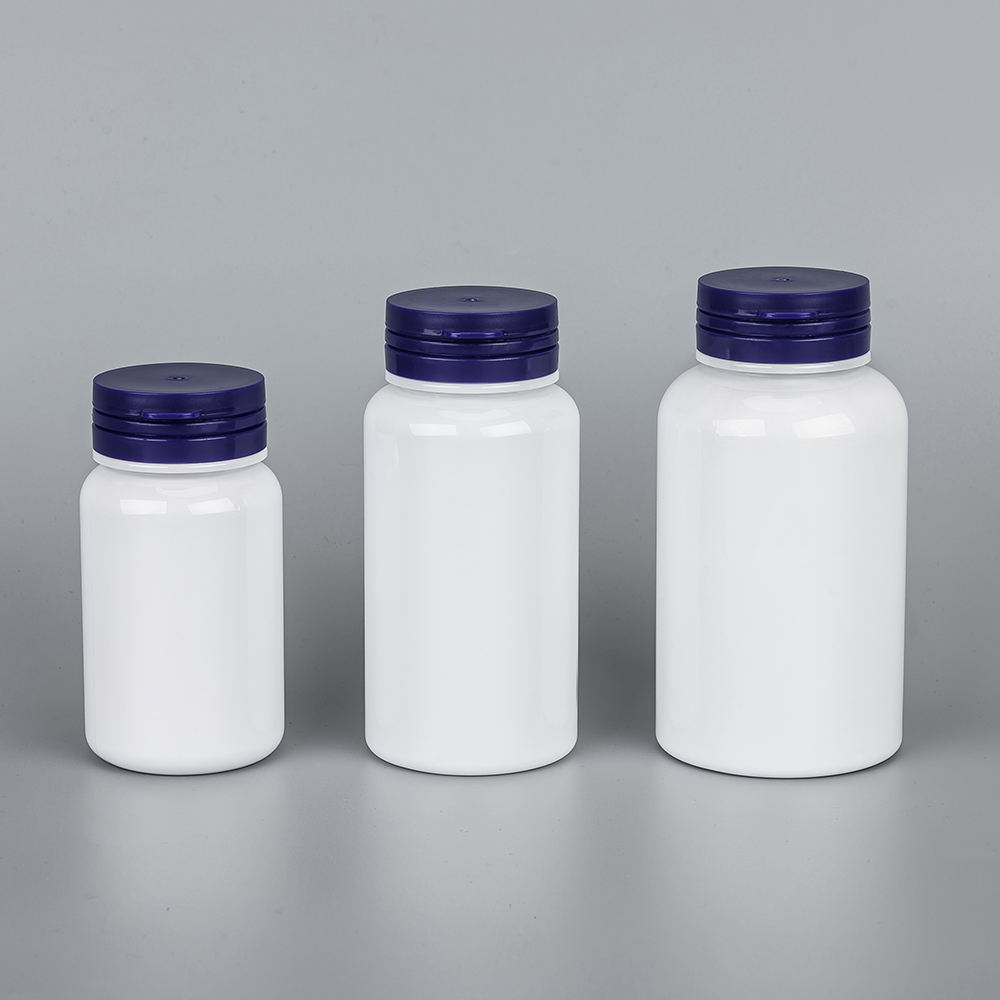
Capsule container manufacturers produce specialized vessels designed to store, protect, and dispense various substances in pharmaceutical, nutraceutical, and industrial applications. These manufacturers focus on creating containers that meet stringent quality standards while maintaining product integrity. The main functions of capsule containers include protecting sensitive contents from environmental degradation, maintaining product potency, and ensuring accurate dosing for end-users. Technologically advanced capsule container manufacturers employ precision engineering and automated production systems to achieve consistent quality. Modern manufacturing processes utilize pharmaceutical-grade materials such as gelatin, vegetarian cellulose, and specialized polymers. These materials undergo rigorous testing to ensure compatibility with diverse formulations and compliance with international regulatory standards. The technological features of leading capsule container manufacturers include size standardization, color customization, and embossing capabilities. Advanced machinery enables tight tolerances and uniform wall thickness throughout production runs. Quality control systems integrate real-time monitoring and inspection protocols to detect defects before packaging occurs. Capsule container manufacturers serve multiple industries including pharmaceuticals, dietary supplements, vitamins, and cosmetics. Applications range from over-the-counter medications to prescription formulations and specialized nutritional products. The versatility of capsule containers makes them preferred solutions for manufacturers seeking reliable, professional packaging that enhances brand perception and consumer confidence in their products.

Popular Products

Capsule container manufacturers deliver substantial operational benefits that extend throughout the supply chain and improve bottom-line results. First, these manufacturers provide superior product protection through engineered designs that shield contents from moisture, light, and oxidation. This protective function significantly extends shelf life and maintains product efficacy, directly reducing waste and increasing profitability for distributors and retailers. Working with reputable capsule container manufacturers ensures compliance with regulatory requirements across multiple markets. Manufacturers maintain certifications including FDA approval, GMP compliance, and international pharmacopeial standards. This regulatory alignment eliminates costly redesign efforts and accelerates market entry for new products. The operational flexibility offered by capsule container manufacturers enables customization without excessive minimum orders or extended lead times. Buyers benefit from color options, size variations, and imprinting capabilities that strengthen brand identity and market differentiation. This customization accessibility allows smaller manufacturers and emerging brands to compete effectively against established competitors. Cost efficiency represents another critical advantage when selecting among capsule container manufacturers. Competitive pricing combined with bulk ordering discounts reduces per-unit expenses significantly. These savings accumulate across production runs, improving margins without compromising quality standards. Reliability and consistency distinguish quality capsule container manufacturers from alternatives. Dependable supply chains and predictable production schedules prevent disruptions that could halt manufacturing operations. Furthermore, capsule container manufacturers offer technical support and formulation guidance, helping customers optimize product performance and address specific packaging challenges effectively.

Tips And Tricks

Why is a wide-mouth supplement container better for powders?

10

Jul

Why is a wide-mouth supplement container better for powders?

When sourcing pharmaceutical or nutraceutical packaging, the physical design of your chosen packaging matters far more than most people realize. The shape, the opening size, and the structural material of a supplement container directly affect how yo...
View More
What are the hidden benefits of an amber medicine bottle design?

28

Aug

What are the hidden benefits of an amber medicine bottle design?

The design of a medicine bottle might seem like a straightforward packaging decision, but the choice to use amber glass in pharmaceutical containers reveals a sophisticated understanding of chemical preservation and consumer protection. An amber medi...
View More
Why should you upgrade your supplement bottle for export markets?

20

Sep

Why should you upgrade your supplement bottle for export markets?

Exporting dietary supplements to international markets requires more than just a quality product inside the container. The supplement bottle you choose directly influences whether your products meet regulatory requirements, survive the supply chain i...
View More
How to source a protein powder container with custom scoops?

22

Sep

How to source a protein powder container with custom scoops?

Sourcing the right protein powder container is a critical decision for supplement brands, fitness companies, and nutritional product manufacturers. The protein powder container serves as both a functional storage solution and a brand ambassador on re...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000

capsule container manufacturers

Premium Material Quality and Safety Standards

Premium Material Quality and Safety Standards

Capsule container manufacturers utilize pharmaceutical-grade materials meeting the highest international safety standards. Leading manufacturers source materials from certified suppliers and implement rigorous quality assurance protocols throughout the supply chain. Each batch undergoes comprehensive testing for purity, contamination, and compatibility with various active ingredients. This meticulous material management ensures capsule containers maintain structural integrity while preventing adverse interactions with contents. Capsule container manufacturers maintain certifications including USP, EP, and BP compliance, guaranteeing that packaging meets stringent pharmaceutical requirements. The investment in premium materials protects consumer health while reducing liability risks for product manufacturers and distributors.
Advanced Production Technology and Precision Engineering

Advanced Production Technology and Precision Engineering

Modern capsule container manufacturers employ state-of-the-art automated equipment delivering exceptional consistency and efficiency. Precision machinery maintains strict tolerances on capsule dimensions, ensuring uniform fitting and sealing across entire production runs. This technological sophistication minimizes defect rates and production waste, reducing overall manufacturing costs. Capsule container manufacturers integrate sophisticated quality control systems utilizing computer vision and automated inspection processes. Real-time monitoring enables immediate detection and correction of production anomalies before they compromise large quantities. Advanced production capabilities allow rapid turnaround times without sacrificing quality, supporting just-in-time inventory management for customers.
Comprehensive Customization and Brand Enhancement Solutions

Comprehensive Customization and Brand Enhancement Solutions

Capsule container manufacturers offer extensive customization options enabling brands to establish distinctive market presence. Choices include diverse color palettes, custom imprinting with logos and product information, and specialized size options for different formulations. This customization flexibility allows companies to create packaging that reflects brand identity and enhances shelf appeal. Capsule container manufacturers collaborate with designers and marketers to develop packaging solutions that communicate product benefits and attract target audiences. The ability to differentiate through customized packaging strengthens consumer recognition and supports premium positioning strategies. These branding solutions provide measurable competitive advantages in crowded retail environments.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000